Machine Symptom Guide
Machine Failure Symptoms: What Is Your Machine Telling You?
Use this guide to match the machine failure symptoms you are seeing to a likely cause, the FPA service that finds and fixes it, the tools behind the diagnosis, and the training that teaches your team to catch it next time. It covers rotating equipment, electrical systems, lubrication, compressed air and the maintenance program itself.
How the guide works
Start with what you see
Find your machine failure symptoms by category
Each of the 17 machine failure symptoms below maps to a service we perform, the tools we use, and the class that builds the skill in-house. Jump to a category:
Urgency key: CALL NOW = safety risk or failure is close · THIS WEEK = diagnose before it gets worse · PLAN IT = fix the program, not one machine
Vibration & noise
Machine failure symptoms: vibration and noise
Machine trips, automatic shutdowns and overloads
What you’ll notice: A machine shuts itself down on a high-vibration alarm, or a motor trips on overload. It often restarts and runs, then trips again hours or days later. You may see rising amps or vibration readings before each trip, and operators start bypassing or raising alarm setpoints just to keep production running.
Likely causes: Unbalance or misalignment that loads the bearings and drives up vibration and current, a failing bearing or coupling, looseness or a rotor rub, running close to a resonance, a binding or fouled driven machine overloading the motor, or a faulty or poorly set vibration trip sensor.
What to do now: Don’t raise or bypass the trip setpoint. Log amps and vibration before each trip, confirm the trip sensor is mounted and reading correctly, and get a vibration analysis before the next restart.
FPA Service
Tools
Training
Fan or rotor shaking at running speed
What you’ll notice: Strong once-per-revolution vibration, often right after cleaning, a repair or product buildup on the wheel.
Likely causes: Mass unbalance from buildup, erosion, lost balance weights or a replaced part.
What to do now: Clean the wheel if you can see buildup, then re-measure the 1x vibration. If it stays high, field balancing in place usually fixes it in one visit without pulling the rotor.
Vibration is high or climbing
What you’ll notice: Overall readings trending up, route alarms, a machine that feels rougher than last month.
Likely causes: Unbalance, misalignment, looseness, bearing wear, resonance.
What to do now: Compare today’s reading with the machine’s baseline and the ISO 20816 zones. Shorten the route interval on that machine and have the spectrum analyzed so the fault is named before it speeds up.
Couplings, seals and bearings keep failing early
What you’ll notice: Short seal life, worn coupling inserts, high axial vibration, a warm coupling guard.
Likely causes: Shaft misalignment, soft foot, pipe strain, thermal growth not accounted for.
What to do now: Stop replacing parts on the same schedule. Check soft foot and pipe strain, then laser align the machine with thermal growth allowed for before the next seal or coupling goes in.
Grinding, squealing or rumbling bearings
What you’ll notice: New noise from a bearing housing, rising high-frequency readings, grease purging from seals.
Likely causes: Lubrication starvation or over-greasing, contamination, early bearing defects.
What to do now: Don’t add grease out of habit. Listen with ultrasound while greasing slowly, stop when the noise level drops, and trend high-frequency vibration to judge how far the defect has progressed.
Structure, piping or base visibly moving
What you’ll notice: You can see the frame, skid, piping or handrail move. Cracked welds or loose anchor bolts.
Likely causes: Structural resonance, looseness, weak foundations, operating near a natural frequency.
What to do now: Check anchor bolts and welds first. If it still moves, a bump test or operating deflection shape study finds the resonance, so you can stiffen or detune the structure instead of guessing.
Heat
Machine failure symptoms: heat
Bearings or housings running hot
What you’ll notice: Housing too hot to touch, rising temperature trend, discolored grease or oil.
Likely causes: Wrong or degraded lubricant, overload, misalignment, failing bearing.
What to do now: Confirm the reading with a thermal camera or contact probe, compare it with sister machines, and check the lubricant type and level. A fast rise or a reading well above normal means plan a shutdown.
Hot electrical panels, breakers or connections
What you’ll notice: Warm panel doors, discolored lugs, a burning smell, nuisance breaker trips.
Likely causes: Loose or corroded connections, overloaded circuits, phase imbalance.
What to do now: Limit access and don’t open energized gear without the PPE and procedures NFPA 70E requires. Get an infrared survey under load to pinpoint the hot connection, then repair it as soon as it can be safely de-energized.
Electrical
Machine failure symptoms: electrical
Motor tripping, overheating or drawing high current
What you’ll notice: Overload trips, hot windings, current imbalance between phases, failed starts.
Likely causes: Insulation breakdown, broken rotor bars, supply problems, mechanical overload.
What to do now: Don’t keep resetting the overload. Record phase currents and voltage, check the driven load for binding, and run motor circuit and current signature tests to separate electrical faults from mechanical ones.
FPA Service
Training
Arcing, buzzing or crackling in switchgear
What you’ll notice: Audible buzzing or crackling, ozone smell, tracking marks on insulators.
Likely causes: Corona, tracking and partial discharge, loose connections.
What to do now: Keep people clear and treat it as an arc-flash hazard. An airborne ultrasound scan from outside the enclosure and an infrared survey through IR windows locate the source without opening the gear.
Standby generator: will it carry the load?
What you’ll notice: Unproven after install or overhaul, high vibration at load, no recent test record.
Likely causes: Untested installation, mount or alignment problems, faults hidden at no-load.
What to do now: Don’t wait for an outage to find out. Schedule vibration testing under load, not just at idle, and keep the results as an acceptance baseline before storm season.
Oil, air & startup
Machine failure symptoms: oil, air and startup
Hissing air or compressors that never unload
What you’ll notice: Audible hissing, compressors running nonstop, pressure drops at the far end of the header.
Likely causes: Leaking fittings, hoses, drains and quick-connects.
What to do now: Run an ultrasound leak survey during production, tag and rank each leak by cost, and fix the biggest first. Re-survey after repairs to confirm the compressor actually unloads.
Training
Oil that is dark, milky, foamy or full of particles
What you’ll notice: Changes in the sight glass, water at the bottom, metal on the drain magnet.
Likely causes: Water or dirt ingress, oxidation, wrong lubricant, internal wear.
What to do now: Pull a sample from a live zone, not the drain, and send it for analysis before you top off. Fit sight glasses and breathers so operators can spot water and dirt between samples.
FPA Service
New pump or machine runs rough after install
What you’ll notice: High vibration from day one, seal leaks in the first weeks, unexplained noise at startup.
Likely causes: Installation misalignment, pipe strain, soft foot, base or grout problems.
What to do now: Before blaming the pump, check alignment, soft foot and pipe strain against the commissioning specs. Record a vibration baseline once it runs smoothly so future readings have something to compare against.
Program & people
Machine failure symptoms in the maintenance program
The same failures keep coming back
What you’ll notice: Repeat work orders on the same assets, reactive maintenance crowding out PMs.
Likely causes: Fixing symptoms instead of root causes, no failure-mode strategy, weak change control.
What to do now: Pick the three assets with the most repeat work orders and run a root cause analysis on each. Then build the monitoring strategy around how those machines actually fail.
Your team can collect data but not read it
What you’ll notice: Readings get taken but nobody acts on them. Experienced people retired and took the know-how with them.
Likely causes: Skill gaps, no certification path, turnover.
What to do now: Run a skill gap assessment, then certify analysts in the technologies you already own. Have FPA review their reports until they can make the call on their own.
Inspection data lives on paper
What you’ll notice: Clipboards, spreadsheets on one laptop, no trend history when something fails.
Likely causes: No mobile workflow, no permanent monitoring on critical assets.
What to do now: Move routes to a mobile app so every reading is time-stamped and trended. Add permanent sensors to critical machines that are hard to reach or need continuous watch.
FPA Service
Training
Fix it now. Own it next time.
Why every symptom links to a class
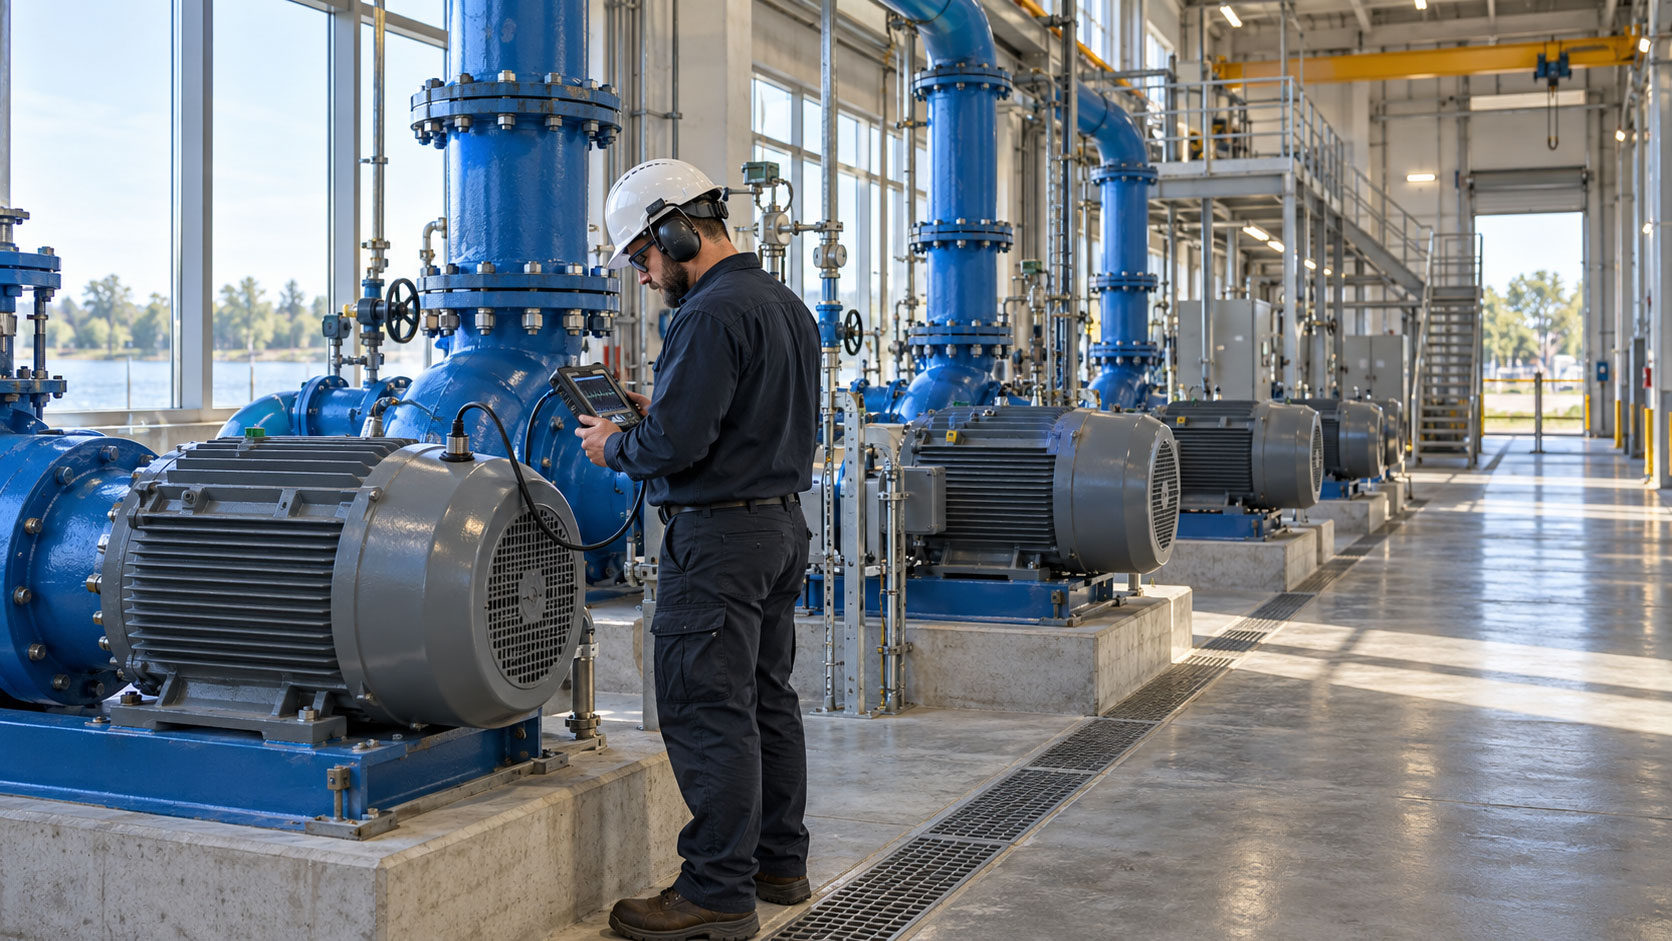
Most machine failure symptoms show up weeks before the breakdown. A service call solves today’s problem. Training stops the next one. Plants that pair FPA field work with in-house skills catch faults earlier, write better work orders, and call us for the hard problems instead of the routine ones.
1. We diagnose
Field services and condition monitoring across Texas, Louisiana and New Mexico, backed by our Houston-area mill test lab.
2. We equip
The same analyzers, cameras, ultrasound and motor testers we use, sized to your plant.
3. We train
Hands-on classes on live machinery, public in Pearland or on-site at your plant.